
 HOTLINE:+8613974960765 +8618507312158 HOTLINE:+8613974960765 +8618507312158


— Knowledge —
— PRODUCTS —
 Service Hotline +8613974960765
Email:susie@hnljpump.com
Mobile:+8618507312158
TEL:+8613974960765
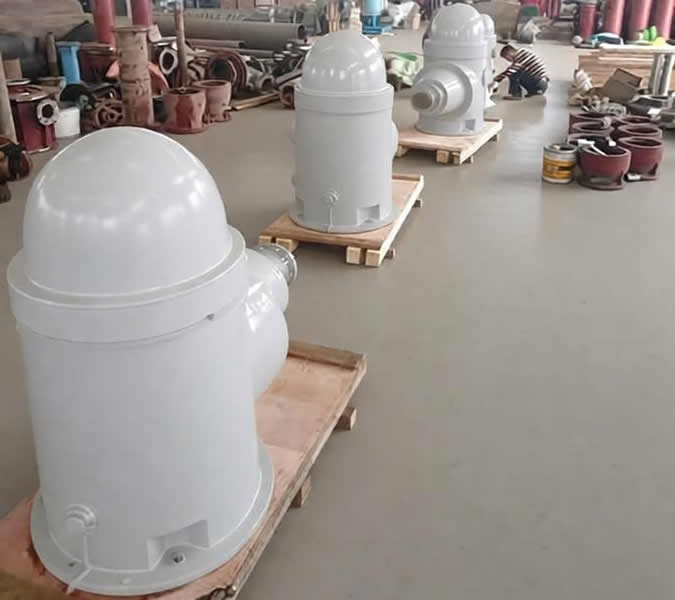
Right Angle Gearboxes
Publication date:2025/3/31 17:53:31 popularity: [content:visits]
The core selection of H-series right angle gearboxes revolves around the actual operating conditions of the pump, matching the three core dimensions of power, axial load, and environmental adaptation to avoid gear breakage, bearing burnout, oil leakage, and other faults caused by parameter mismatch, ensuring the long-term stable operation of the pump system.
This is the core basis for selecting H series right angle gearboxes for pumps. All parameters must be based on the actual operating data of the pump and cannot be directly copied from the rated parameters of the motor
1. Reserve of rated power redundancy: Based on the rated shaft power of the pump, reserve 15%~20% of power redundancy. The rated input power of the right angle gearbox must be greater than the maximum operating shaft power of the pump to avoid early gear wear caused by long-term full load operation. The adaptive power range covers 0~1520HP (approximately 1120kW), which can meet the full power range requirements from small agricultural pumps to large industrial pumps.
2. Torque condition coefficient correction: Multiply the load characteristics of the pump by the corresponding condition coefficient KA to calculate the required rated torque after correction:
·Stable load (clear water centrifugal pump): KA=1.0~1.2
·Medium impact load (axial flow pump, fire pump): KA=1.5~1.75
·Heavy load impact load (mine drainage pump, mud pump): KA=2.0~2.5
After correction, the rated torque of the right angle gearbox must be ≥ the required torque of the pump × KA, and the peak starting torque of the pump must not exceed the instantaneous maximum bearing torque of the gearbox (usually 2-3 times the rated torque).
3. Accurate calculation of speed and transmission ratio: Based on the rated speed of the prime mover and the required rated speed of the pump, calculate the theoretical transmission ratio, and prioritize the use of the gearbox standard transmission ratio sequence (speed increase ratio 1:1~1:2, speed decrease ratio 4:1~11:10) to avoid significant cost increases caused by non-standard customization. At the same time, it is necessary to ensure that the input speed of the prime mover is ≤ the upper limit of the input speed of the gearbox (conventional models ≤ 1500r/min). Overloading operation will directly lead to lubrication failure and cause dry grinding of the tooth surface.
⚙️ Verification of axial thrust bearing capacity
This is the core selection dimension that distinguishes the H-series right angle gearbox for pumps from ordinary right angle gearboxes, which directly determines the service life of the equipment:
1. The maximum axial thrust of the actual operation of the pump must be taken as the benchmark, and the rated axial thrust bearing capacity of the gearbox must be ≥ 1.2 times the maximum axial thrust of the pump. The maximum axial thrust of the conventional H series model can reach 125000N, which can directly bear all axial loads of the vertical pump during start stop and variable operating conditions, greatly simplifying the thrust bearing structure of the pump body itself.
Under the working conditions of high head deep well pumps and long shaft pumps, the axial thrust will increase exponentially with the increase of head. It is prohibited to directly use ordinary right angle gearboxes of the same power. The corresponding high thrust model must be upgraded, otherwise there will be thrust bearing burnout and output shaft displacement exceeding the standard within 3 months.
Based on the actual usage environment on site, customized configurations are made to avoid the inability of H-series right angle gearboxes for general-purpose pumps to adapt to special working conditions
1. Adaptation to extreme temperature scenarios:
·High temperature environment (ambient temperature>40 ℃): It is necessary to choose a model with an external forced circulation cooler, matched with L-CKD320 high viscosity heavy-duty gear oil, to avoid sealing failure caused by high oil temperature.
·Low temperature environment (ambient temperature<-10 ℃): An electric heating preheating device must be equipped, and low-temperature synthetic gear oil should be selected to prevent the lubricating oil from solidifying at low temperatures and causing damage to the gears during dry grinding at the moment of start-up.
2. Protection level matching:
·Ordinary indoor pump room scenario: Choosing IP54 standard protection level can meet the requirements.
·Outdoor environments with high dust, high salt spray at the seaside, and chemical corrosion: must be upgraded to IP55 or above protection level. The shaft end should be sealed with fluorine rubber double lips, and the surface of the shell should be treated with anti-corrosion spray to prevent corrosion and dust from entering the interior.
3. Confirmation of installation method:
·Vertical inverted and narrow space wall mounted installation: It is necessary to confirm in advance that the H-series right angle gearbox for the pump supports the corresponding installation method, and is equipped with a special leak proof oil sealing structure to avoid lubricating oil leakage faults in non-standard installation positions.
1. Matching of shaft diameter and coupling: Check the output shaft diameter of the prime mover and the input shaft diameter of the pump one by one, and ensure that they match the standard hole diameter of the gearbox input and output ends completely to avoid forced hole expansion or contraction, which may cause installation stress concentration and result in excessive shaft vibration during operation.
2. Confirmation of lubrication system selection: For high-power models with input power exceeding 200kW, the use of basic splash lubrication structure is prohibited. It must be upgraded to a forced oil injection lubrication system, equipped with oil level and oil temperature online monitoring sensors to monitor the operating status in real time and predict faults in advance.
3. Customized adaptation for special working conditions: For models used in chemical explosion-proof areas, explosion-proof configurations must be selected, and all electrical monitoring components must meet the Exd II CT4 explosion-proof level requirements, fully complying with safety regulations in the petrochemical industry.
⚠️ Core experience in selecting and avoiding pitfalls
1. It is prohibited to directly use the rated power of the motor as the sole selection basis. The working condition coefficient and axial thrust parameters of the pump must be superimposed, otherwise overload faults may occur when small horses pull large vehicles.
2. Under normal operating conditions, ordinary clean water pumps do not need to blindly choose imported high-end models. The domestically produced standard H series right angle gearbox has the highest cost-effectiveness, with procurement costs only one-third of imported products, fully meeting the long-term stable operation needs.
3. Long term operation with excessive axial thrust is strictly prohibited. Even short-term overload can significantly shorten the life of the thrust bearing and directly cause major equipment damage.
Related Recommendations

Service hotline
screenshots ,WeChat Scan the Qr Code
WeChat:ljpump6666